How to Choose a Hi Vis Clothing Manufacturer for Your Business
Moving beyond basic compliance certificates: A strategic framework for brand managers, distributors, and safety directors to evaluate long-term supply chain consistency, technical integration, and manufacturing capability.
Executive Summary: Selecting the Right Manufacturer
To choose the right high-visibility clothing manufacturer, evaluate beyond baseline price and single lab certificates by auditing vertical integration capabilities, in-house real-time quality control, and engineering-level ODM design support. A qualified manufacturing partner must control both retroreflective material synthesis and precision technical apparel assembly, operate structured IQC/PQC/FQC batch-testing protocols to ensure photometric consistency past 25–50 wash cycles, and maintain globally recognized ISO 9001, BSCI, ANSI/ISEA 107, EN ISO 20471, and OEKO-TEX Standard 100 accreditations to protect your brand from operational liability and supply chain disruption.
Table of Contents
- 1. The Strategic Reality: Vendor vs. Partner
- 2. Escaping the “Golden Sample” & Test Report Trap
- 3. The Power of Full Vertical Integration
- 4. Evaluating True ODM Engineering Capacity
- 5. 2026 Standards: Sustainability & Traceability
- 6. The 5-Point B2B Factory Audit Checklist
- 7. Frequently Asked Questions
1. The Strategic Reality: Choosing a Safety Partner, Not Just a Vendor
For enterprise PPE distributors, utility program managers, and private safety labels, workwear sourcing cannot be treated as a generic commodities transaction. A defective run of t-shirts causes inconvenience; a batch of non-compliant high-visibility jackets causes catastrophic occupational safety failure, regulatory stop-work orders, and devastating product recalls under standards governed by organizations like the U.S. Occupational Safety and Health Administration (OSHA).
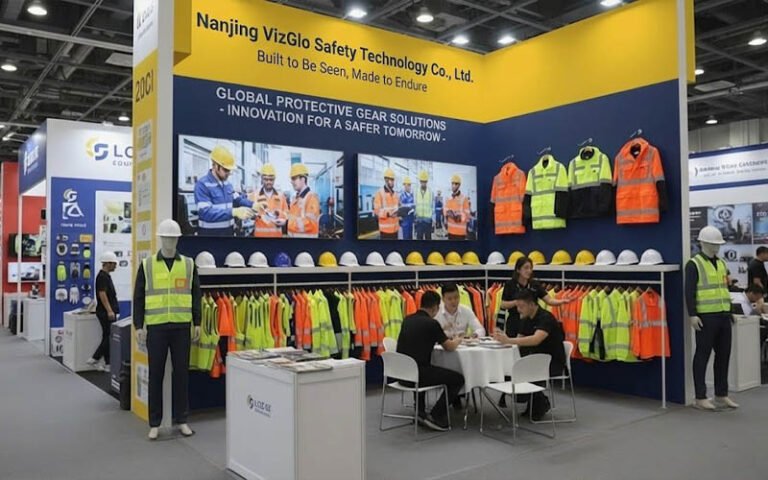
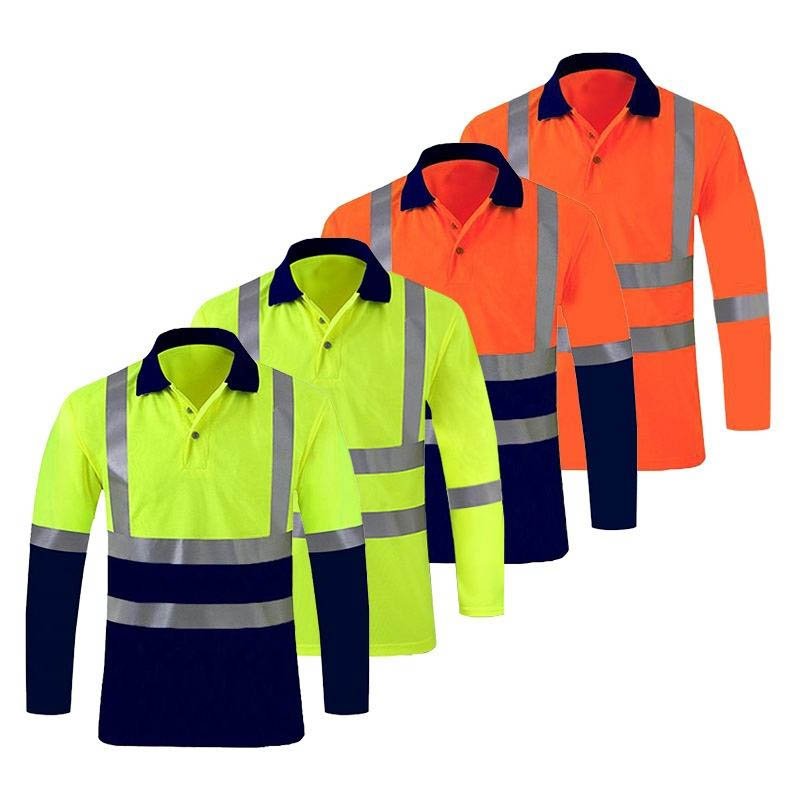
When identifying a manufacturing partner, leading apparel programs assess a supplier’s core capabilities in raw material testing, ergonomic tailoring, and regulatory alignment across target export territories. Whether you are expanding an existing commercial catalog or developing an entirely new enterprise range, exploring specialized production lines via our dedicated Hi Vis Clothing Manufacturing Division ensures consistent compliance and production integrity.

2. Escaping the “Golden Sample” & Test Report Trap
Every international sourcing director has experienced the “Golden Sample” phenomenon: an overseas supplier submits an impeccable prototype complete with an authentic third-party testing report. Yet, when the container-load bulk order arrives, garments show premature micro-cracking, delaminating heat transfers, or fluorescent background fading after merely three industrial wash cycles.
The reality is that any workshop can purchase premium components to produce a single compliant test piece. The true benchmark of industrial excellence is manufacturing consistency—ensuring the 50,000th production piece delivers the exact coefficient of retroreflection ($R_A \ge 330\text{ cd}/(\text{lx}\cdot\text{m}^2)$) and chromaticity coordinates as the initial prototype.
In-house spectral testing for fluorescent fabric dyes and photometric micro-bead concentration before bulk cutting begins.
Continuous calibrated monitoring of seam tension, heat-seal pressure/dwell time, and waterproof tape welding.
Batch-level accelerated washing trials, tensile load testing, and dimensional stability checks prior to export container loading.
Always ask prospective manufacturers: “Do you operate an on-site testing lab to verify retroreflection and colorfastness in real-time, or do you rely strictly on external annual certificates?”
3. The Decisive Advantage: Full Vertical Integration
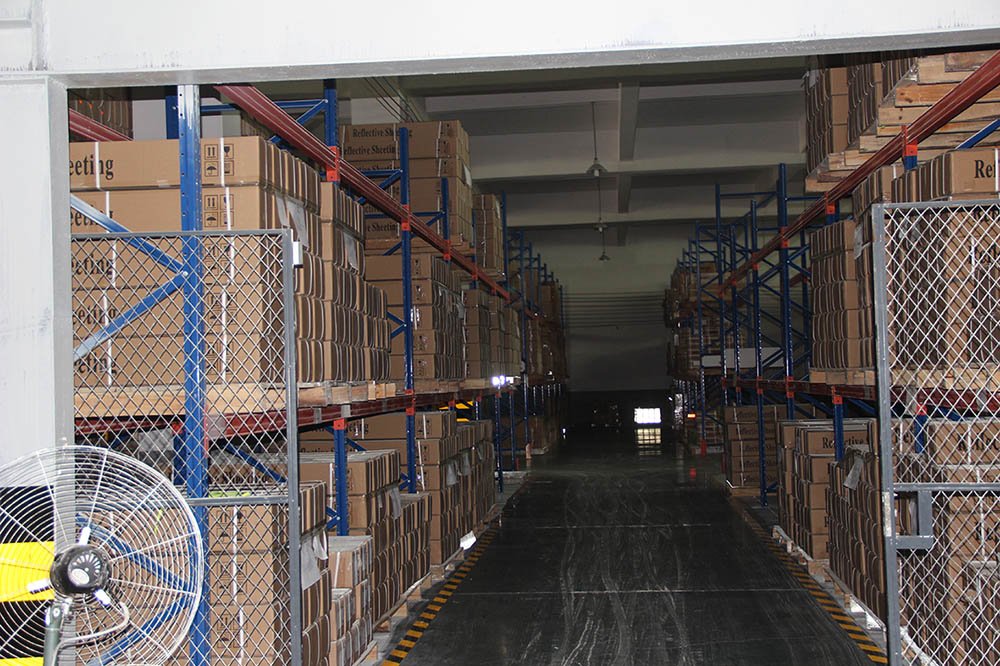
The typical PPE supply chain is fractured. Traditional cut-and-sew workshops act as mere component aggregators, sourcing fluorescent shell fabrics from one mill, retroreflective trims from a middleman, and hardware from another vendor. When problems like bonding failure or premature reflectivity decay arise, suppliers shift blame across their unintegrated vendors.
Choosing a vertically integrated manufacturer that directly manufactures both the core retroreflective technology and the finished apparel provides distinct strategic advantages:
Seamless Chemical and Thermal Compatibility
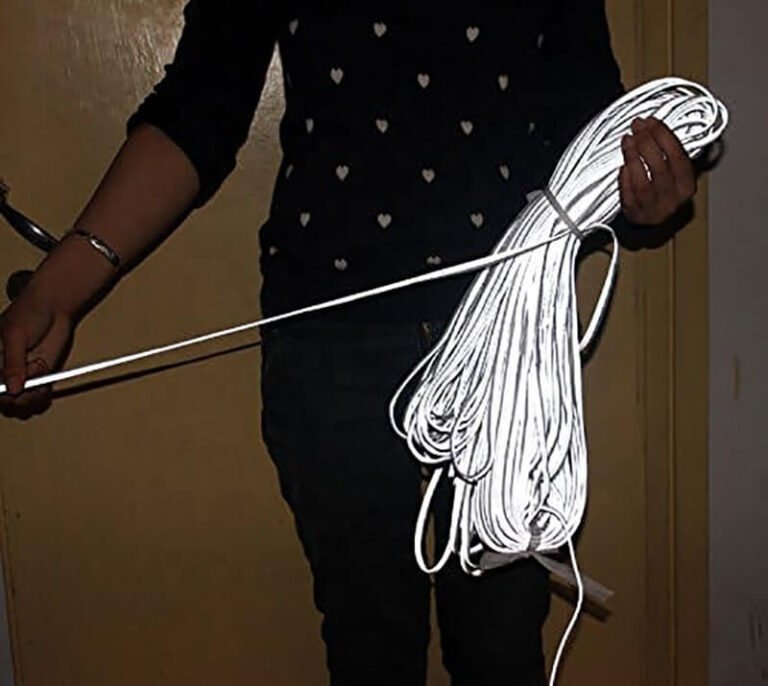
Retroreflective tapes and segmented films engineered alongside specific base textiles eliminate polymer adhesive mismatches, ensuring performance exceeding 25 to 50 ISO 6330 washing cycles.
Unrestricted Component-Level Customization
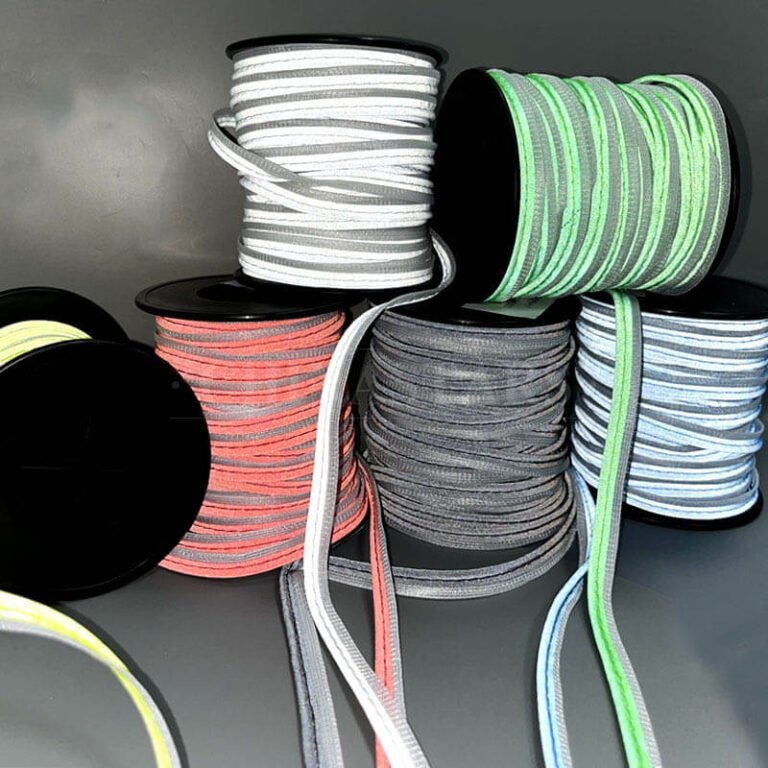
Direct access to raw synthesis allows tailored custom solutions—from specific base fabrics (TC, Polyester, Spandex) to unique reflective patterns—without waiting for third-party R&D cycles. Review our specialized technical capabilities across our Reflective Material Division.
Uncompromised Supply Chain Security
By eliminating trim brokers and intermediary margins, vertical integration insulates procurement programs from upstream production delays and volatile price shocks.
4. Distinguishing Between an Order-Taker and an OEM/ODM Engineering Partner
A low-tier OEM factory acts merely as an order-taker: they receive your tech pack, produce garments without review, and pass every design flaw directly to your inventory. In contrast, an engineering-driven ODM partner optimizes your products for compliance, durability, and practical field performance.
| Evaluation Metric | Transactional Supplier (Order-Taker) | Strategic ODM/OEM Partner |
|---|---|---|
| Tech Pack Review | Quotes blindly without assessing standards | Identifies Class 2 vs Class 3 compliance risks and optimization areas |
| Trim Selection | Applies standard, generic rigid tapes | Recommends segmented, breathable, or elastic films matched to garment usage |
| Custom Branding | Basic silk-screen transfers prone to cracking | Engineered industrial heat-applied retroreflective brand graphics |
| Proactive R&D | None; relies on client requests | Provides proprietary lightweight fabrics, high-flex trims, and sustainable finishes |
True technical competence requires seasoned pattern makers and industrial designers who understand international compliance frameworks, such as European Committee for Standardization (CEN) protocols and ANSI body-coverage geometry. Discover how our technical team executes tailored enterprise specifications via our Customization (OEM/ODM) Solutions.
5. Forward-Looking Compliance: Sustainability & Ethical Governance
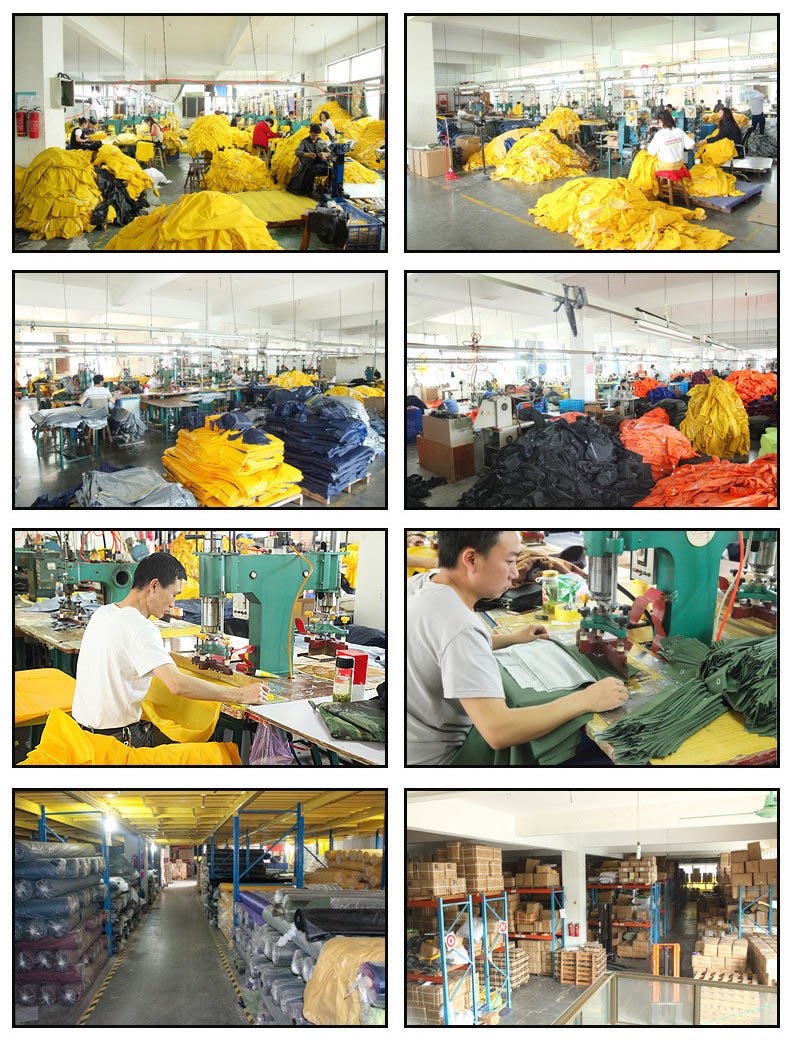
Modern procurement strategies place heavy emphasis on ethical production and circular chemistry. Global supply chain legislation—such as the EU Corporate Sustainability Due Diligence Directive—mandates rigorous tier-1 and tier-2 vendor auditing. Sourcing from non-compliant facilities introduces severe regulatory and reputational risk.
Eco-Friendly Material Selection
Verification of GRS-certified recycled polyester yarns (rPET), bio-based polyurethane membranes, and fluorocarbon-free (PFC-Free DWR) water-repellent coatings.
Chemical Safety Certification
Audited compliance with OEKO-TEX Standard 100 parameters, ensuring all dyes, trims, and adhesives remain free from hazardous aromatic amines and heavy metals.
Social Responsibility Audits
Active participation in third-party workplace safety, fair compensation, and environmental management programs verified by BSCI or Sedex SMETA.
Total Quality Governance
Certified ISO 9001 quality management architecture ensuring full documentation, traceability, and batch control across every production lot.
6. The 5-Point B2B Factory Audit Checklist
When qualifying a prospective manufacturing partner via on-site visit or remote technical audit, focus on these five core capability indicators:
- Raw Material Control & Testing: Does the facility maintain calibrated retroreflectometers and spectrophotometers on-site to inspect every roll of textile and reflective material upon delivery?
- Seam & Thermal Bonding Verification: For technical outerwear and rainwear, what automated testing is performed to ensure seam-seal hydrostatic resistance exceeds 10,000 mm $H_2O$?
- Component Lineage & Supply Integration: Does the factory synthesize its own reflective media, or are they entirely reliant on third-party trim brokers for supply continuity?
- Standard-Specific Design Expertise: Can the engineering team demonstrate proper compliance with ANSI/ISEA 107, EN ISO 20471, and AS/NZS 1906.4 sizing and layout requirements across smallest (XS/S) sizes?
- Traceability & Batch Accountability: Is every production batch coded with serial identifiers linking finished garments directly back to raw polymer and dye lot inspections?
Frequently Asked Questions (FAQ)
Why is vertical integration critical in hi vis garment manufacturing?
How can buyers avoid the “Golden Sample” trap when auditing factories?
What certifications should a reputable hi-vis manufacturer maintain for global markets?
What is the key difference between a cut-and-sew vendor and an ODM partner?
Partner with a Vertically Integrated Safety Manufacturer
Nanjing VizGlo Safety delivers certified high-visibility workwear and proprietary retroreflective materials for global brands, rail operators, and tier-1 distributors. Experience end-to-end consistency from raw bead to finished garment.